Dignified Separation Technology
Membrane technology has become a dignified separation technology over the past decennia. The main force of membrane technology is the fact that it works without the addition of chemicals, with a relatively low energy use and easy and well-arranged process conductions.
Membrane technology is a generic term for a number of different, very characteristic separation processes. These processes are of the same kind, because in each of them a membrane is used. Membranes are used more and more often for the creation of process water from groundwater, surface water or wastewater. Membranes are now competitive for conventional techniques.
The membrane separation process is based on the presence of semi permeable membranes. The principle is quite simple: the membrane acts as a very specific filter that will let water flow through, while it catches suspended solids and other substances.
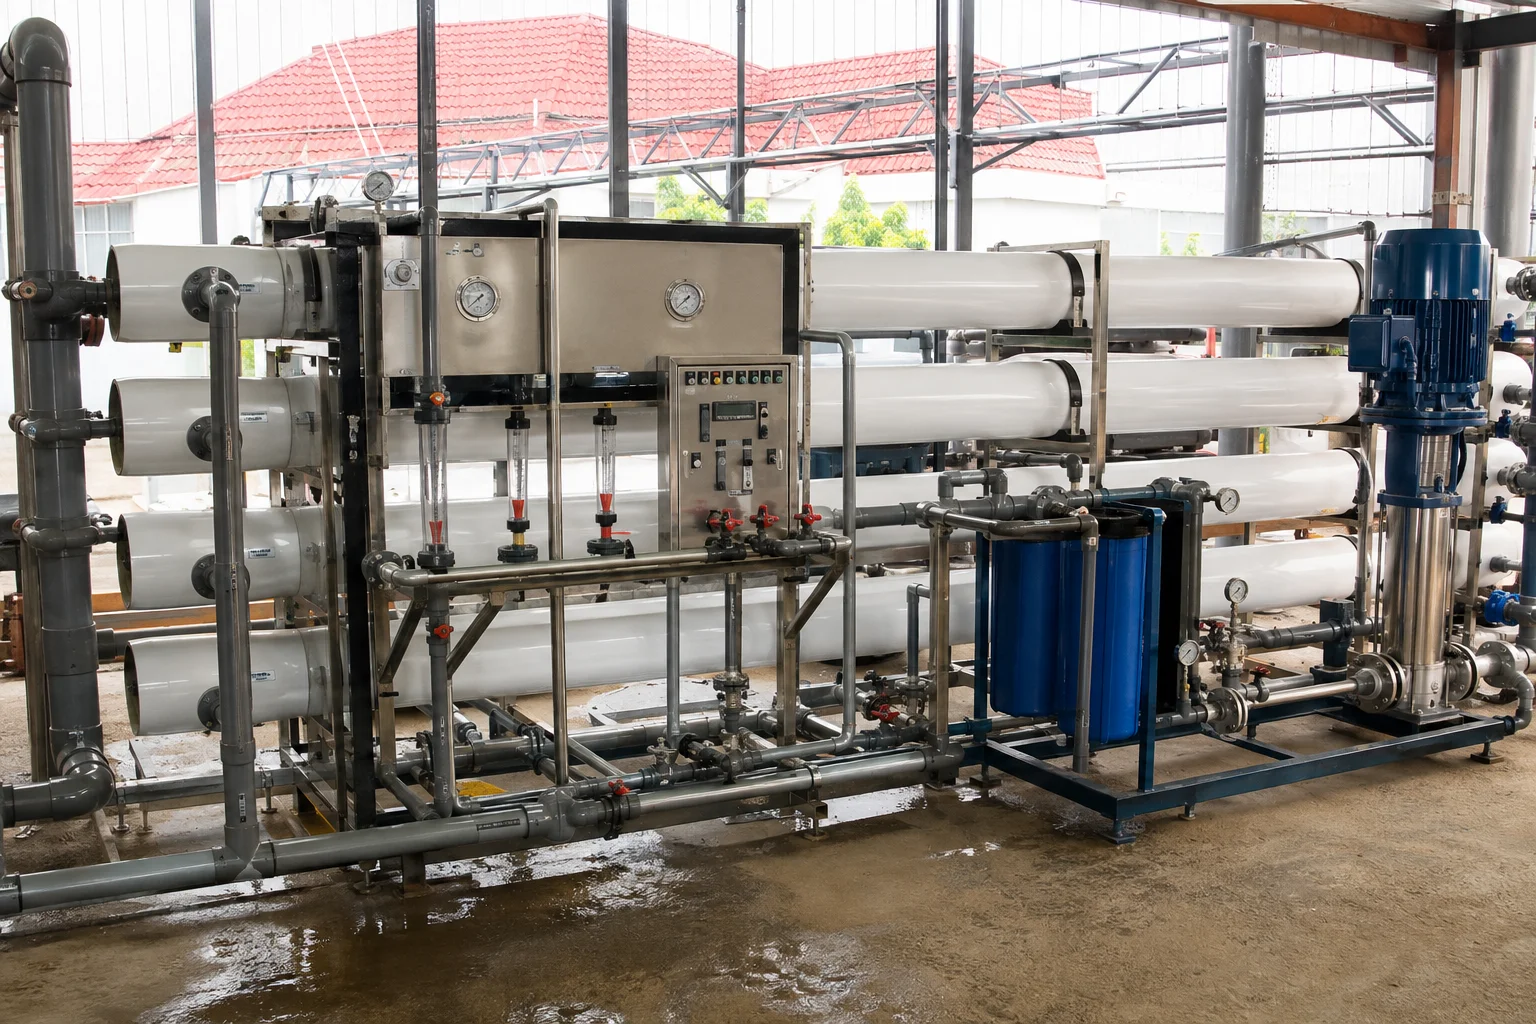
Comprehensive Benefits
- Non Thermal
- No Phase Change
- No Chemical Reaction
- Simple in Concept and Operation
- Modular and Easy to Scale-up
- Low Energy Consumption
- Environmental Friendly
- Recovery and Reuse of Byproducts
- Permit Drastic Improvements in Manufacturing
- Substantial Reduction in Equipment Size
- Provide Cheaper and Sustainable Solutions
- High Quality of Final Products
- No Moving Parts
- Operational Flexibility
- Portability (where required)
- Flexibility for Automation and Remote Control
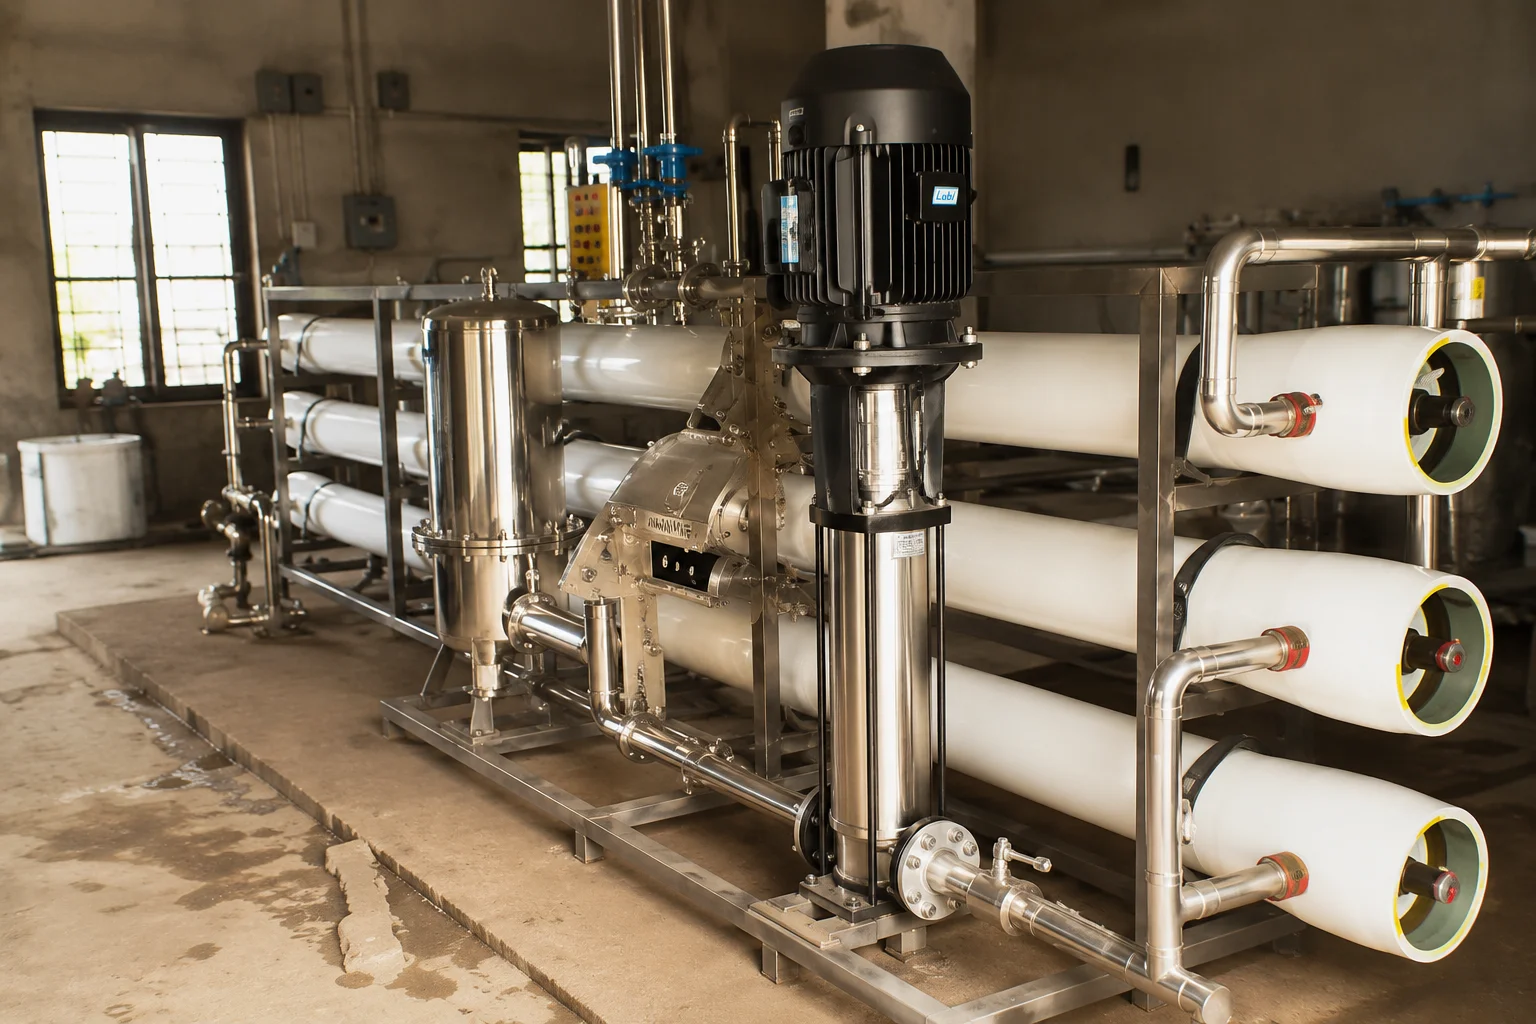
UF Applications
Degreasing Processes
Metal Particle Recovery
Metal Plating Wastewater Treatment
Removal of Non-Toxic degradable pollutants such as proteins and other macromolecular compounds and toxic non-degradable components, e.g. dyes and paints, with molecular weights greater than 1000
Tertiary Treatment of the Effluent from Activated Sludge Process
Segregation of Oil/Water Emulsions
Separation of Heavy Metals after Complexation or Precipitation
Pretreatment step prior to RO and Ion Exchang
RO Applications
Desalination
Final Removal of Toxic Components
Degradable Components, if biological treatment is not possible
Post Treatment of the permeate from Ion Exchange and GAC Adsorption.
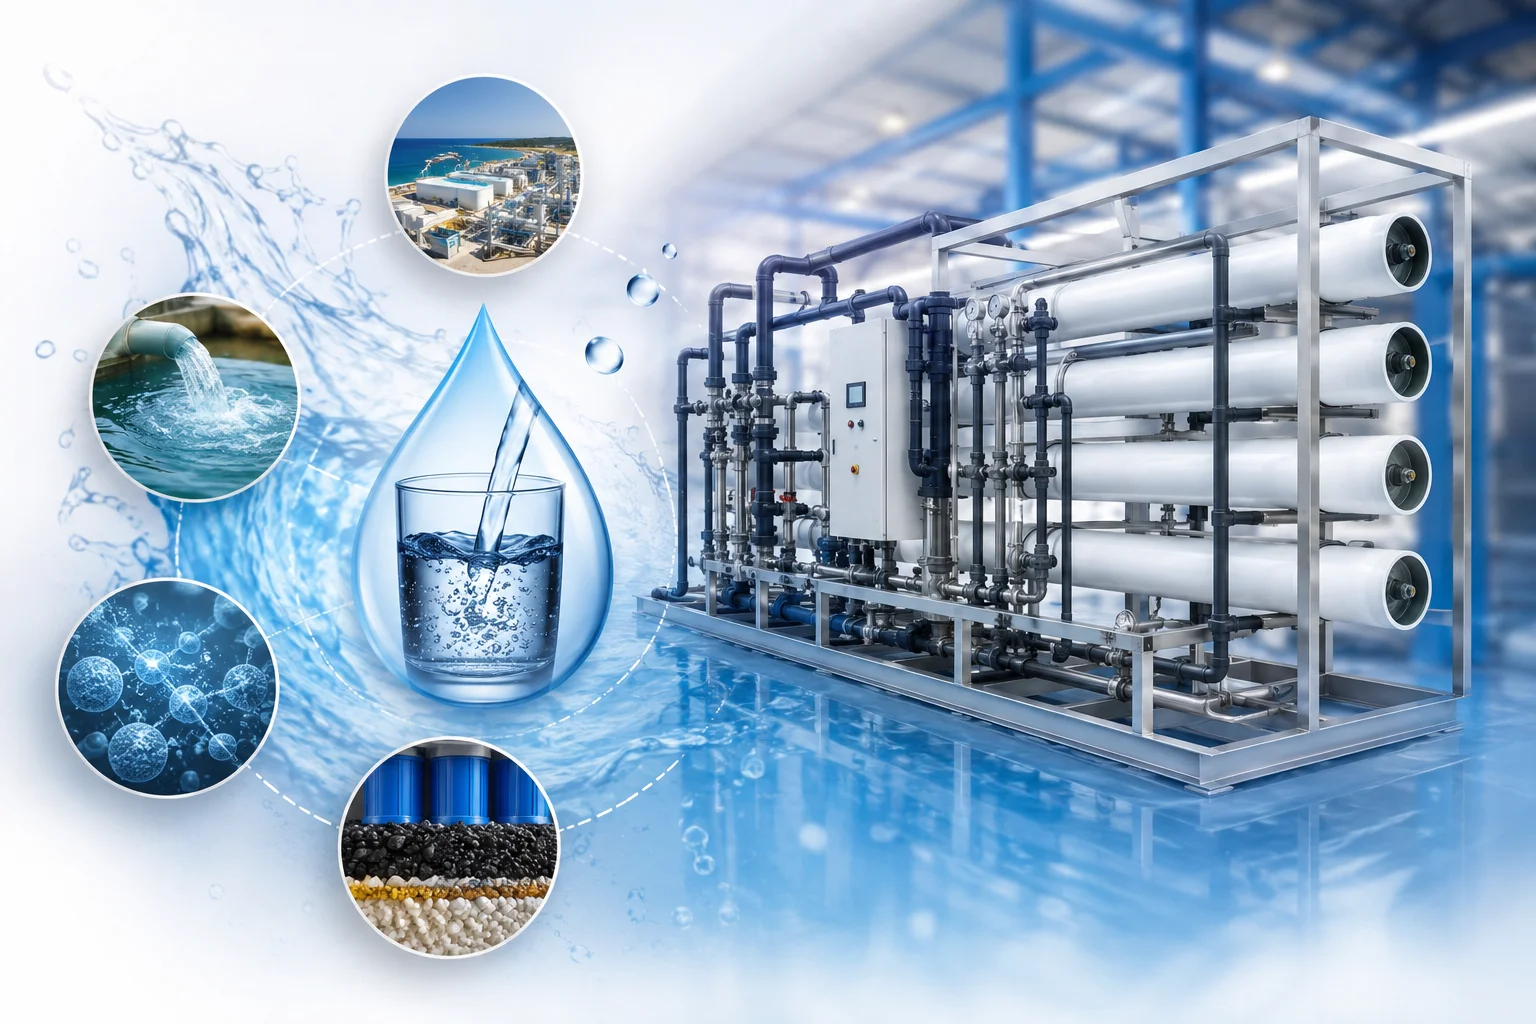
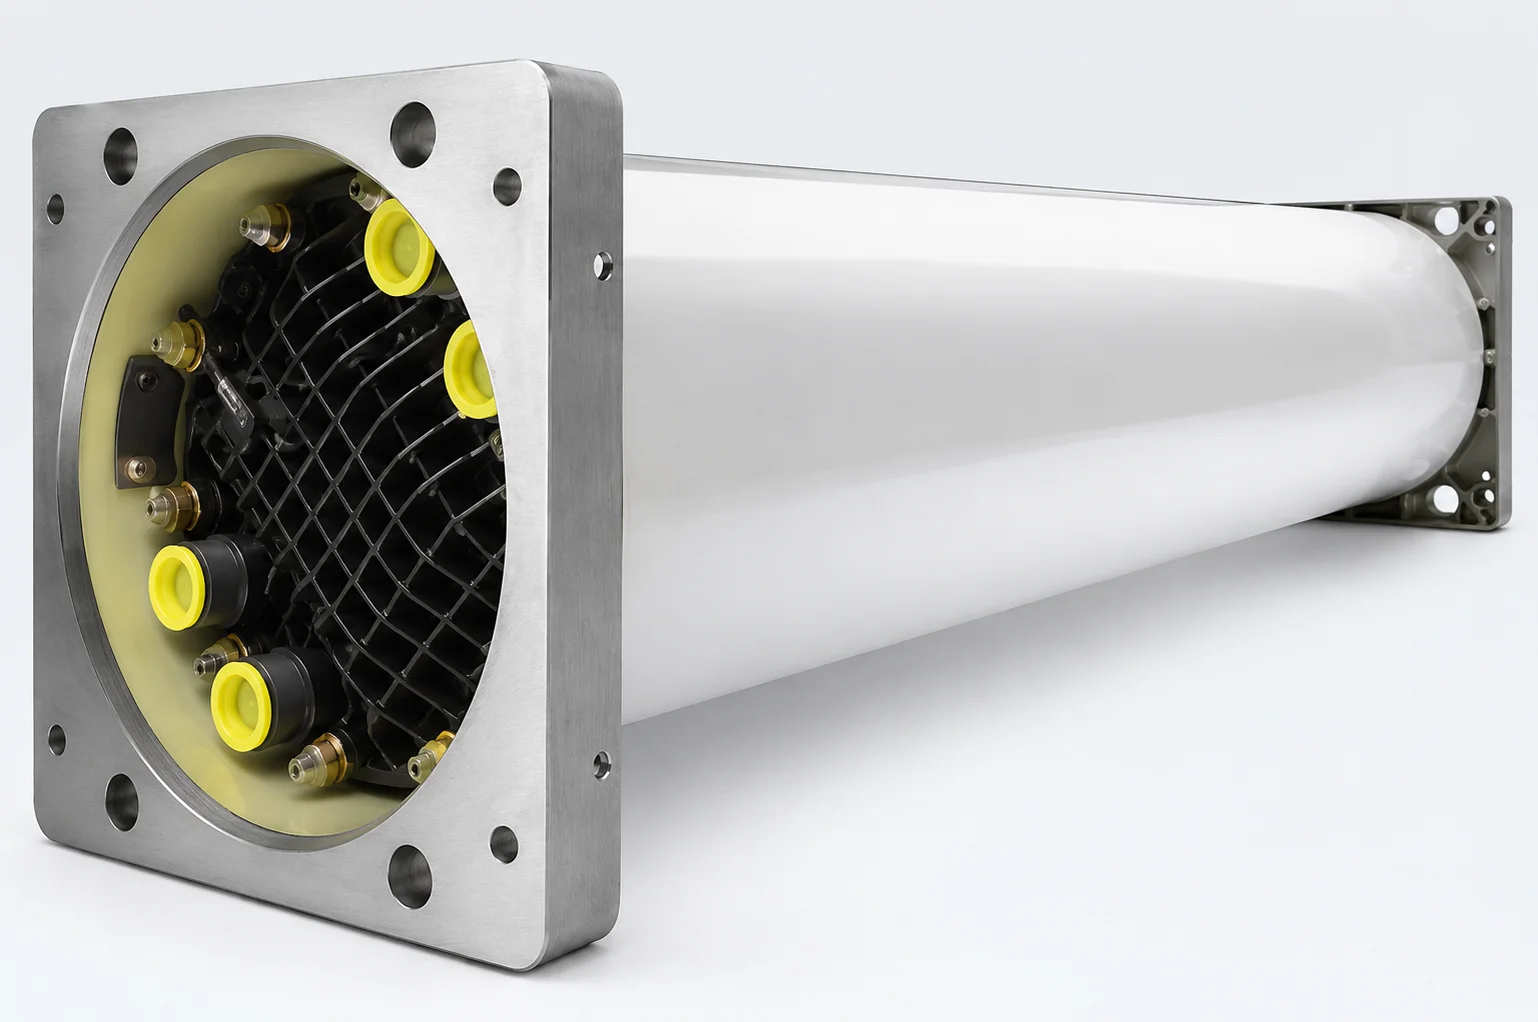
EDI Applications
EDI is useful for any application that requires constant and economic removal of water impurities without using dangerous chemical. Some examples are:
Reuse of residual water in food and beverages industry
Chemical production
Biotechnology
Electronics
Cosmetic
Laboratories
Pharmaceutical industry
Boiler Feed Water
Reduction of ionizable SiO2 and TOC
EDI vs Traditional Ion Exchange
As a substitute for the more traditional ion-exchange process, EDI brings advances in both energy and operating expenses to the high purity water treatment train. By eliminating the periodic regeneration requirement of ion exchange resin, environmental benefits are also realized by avoiding the handling and processing of acid and caustic chemicals brought to the site.
Some of the advantages of the EDI as opposed to the conventional systems of ionic interchange are:
Simple and continuous operation
Chemicals for regeneration completely eliminated
Cost effective operation and maintenance
Low power consumption
Non pollution, safety and reliability
It requires very few automatic valves or complex control sequences that need supervision by an operator
It requires little space
It produces high pure water in a constant flow
It provides complete removal of dissolved inorganic particles
In combination with reverse osmosis pre-treatment, it removes more than 99.9% of ions from the water
Key Performance Metrics
Removal of dissolved inorganic particles
Ion removal with RO pre-treatment
Flow rate and quality output